 24 Hour Service
- 800.825.3222
- Now Hiring
- Request A Quote
China Top Aerosol Can Parts Cone And Dome Manufacturers?
China has become a significant sourcing market for Aerosol Can Parts Cone And Dome, supported by metal-forming experience, broad supplier networks, and competitive production capacity. However, factory selection should involve more than price comparisons. The cone and dome influence can strength, valve fit, crimping performance, appearance, and filling-line stability.
Michael B. O’Rourke, an aerosol packaging engineer with manufacturing experience, once observed, “A small forming error can become a large sealing problem.” That practical warning deserves attention. A reliable manufacturer should explain its steel grades, drawing depth, thickness tolerance, tooling control, and inspection process. Ask for dimensional reports, sample parts, and evidence of production consistency.
Details matter.
A well-made dome should show a clean curve, even wall thickness, and no visible wrinkles around the shoulder. A cone needs accurate geometry, stable neck dimensions, and a surface prepared for dependable assembly. During factory evaluation, buyers can review presses, molds, leak-testing equipment, coating lines, and final inspection records. Clear communication also matters when drawings use different measurement standards.
Still, no supplier is perfect. Even experienced plants may face tooling wear, material variation, or occasional delivery pressure. That is where corrective-action records become valuable. Manufacturers that openly discuss defects often appear more trustworthy than those promising flawless production. This guide examines China’s leading Aerosol Can Parts Cone And Dome manufacturers through technical capability, quality control, customization, certifications, lead times, and export support. The goal is not to promote the cheapest option. It is to identify the partner most capable of producing safe, consistent, and application-ready components.
Aerosol Can Cones and Domes: Functions, Types, and Key Features
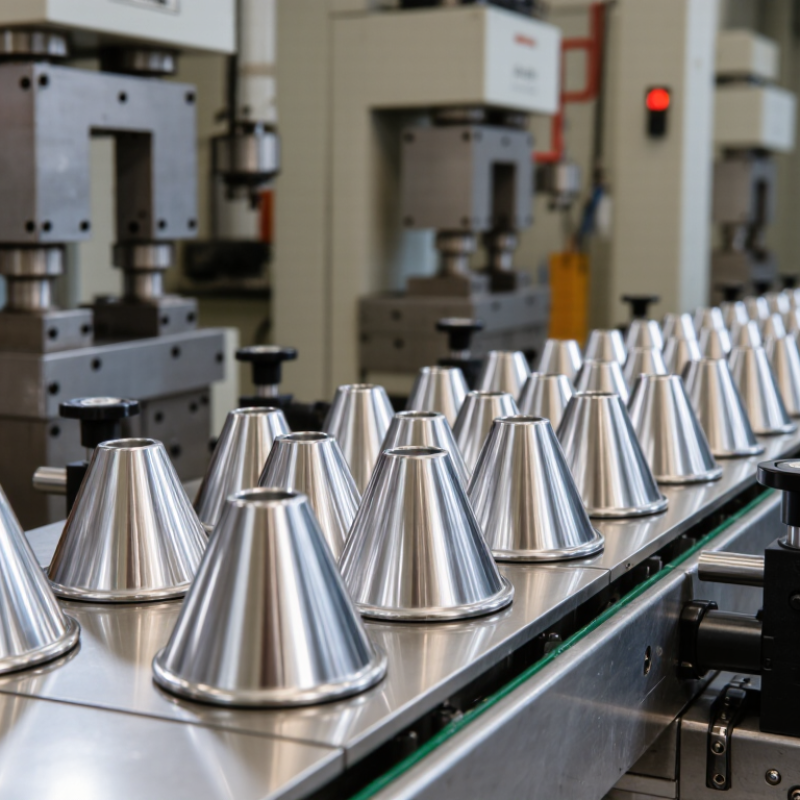
Aerosol can cones and domes are formed metal parts that shape the container’s shoulder and upper structure. The cone connects the cylindrical body to the valve area. It supports pressure distribution and helps create a clean mounting surface. The dome provides a rounded top, improving strength and reducing sharp stress points. Small dimensional errors can affect crimping and sealing.
Common types include shallow cones, deep cones, standard domes, and reinforced domes. The best choice depends on can diameter, product pressure, valve design, and filling conditions. Steel offers high strength and stable forming performance. Aluminum provides lighter weight and strong corrosion resistance. Surface coatings can improve appearance and protect the metal from chemical contact.
Reliable manufacturers in China should control material thickness, forming depth, neck dimensions, and edge quality. In-process gauges and pressure testing support consistent production. Clean surfaces also matter, especially around the valve opening. A practical inspection should check both samples and production records. A perfect drawing can still produce poor parts. Tool wear, uneven lubrication, or slight material variation may change the final shape. Buyers should request test reports, dimensional samples, and clear tolerance data before approving large orders.
| Component Type | Primary Function | Common Material | Typical Manufacturing Process | Typical Size Range | Key Performance Features | Common Applications |
|---|---|---|---|---|---|---|
| Standard Cone | Connects the can body to the valve cup and guides the actuator and valve assembly. | Tinplate, electrolytic chromium-coated steel, or aluminum. | Deep drawing, forming, trimming, curling, and compound flanging. | Designed for nominal can diameters of approximately 35–76 mm. | Accurate valve-cup fit, stable flange, good dimensional repeatability, and compatibility with crimped valve systems. | Personal care, household products, air fresheners, and general industrial aerosols. |
| Low-Profile Cone | Reduces the overall package height while providing the required valve and actuator interface. | Aluminum or tinplate, selected according to pressure and corrosion requirements. | Progressive forming or deep drawing with controlled neck and flange geometry. | Generally used on short packages with can diameters of approximately 45–65 mm. | Compact appearance, lower material usage, efficient palletization, and controlled valve alignment. | Travel-size products, compact personal-care aerosols, and promotional packaging. |
| High-Neck Cone | Provides additional clearance around the actuator and supports tall or specialized valve assemblies. | Tinplate or aluminum with an internal or external protective coating when required. | Multi-stage drawing, necking, curling, and precision flanging. | Typically used with can diameters of approximately 45–76 mm. | Increased actuator clearance, improved component separation, and suitability for specialized dispensing systems. | Foaming products, cosmetic mousses, technical sprays, and products requiring elevated valve geometry. |
| Decorative Cone | Combines the structural function of a cone with a visible surface for printed or embossed decoration. | Pre-printed tinplate, coated steel, or lacquered aluminum. | Forming after printing or coating, followed by trimming, curling, and flange forming. | Available for many standard can diameters, commonly approximately 45–76 mm. | High visual impact, controlled print registration, scratch resistance, and compatibility with retail packaging. | Beauty, personal care, household, and branded consumer aerosol products. |
| Standard Dome | Closes the lower end of the can and distributes internal pressure into the can wall. | Tinplate or aluminum; coating selection depends on product compatibility. | Deep drawing, doming, trimming, curling, and bottom-profile forming. | Commonly matched to can diameters of approximately 35–76 mm. | Pressure resistance, stable bottom geometry, reliable attachment to the can body, and efficient load distribution. | Most pressurized aerosol products, including sprays, foams, and mists. |
| Pressure-Optimized Dome | Improves resistance to internal pressure and helps maintain package integrity during filling, storage, and transport. | Steel or aluminum with controlled thickness and protective internal coating. | Precision deep drawing with optimized radius, base profile, and dimensional controls. | Selected according to can diameter and required working pressure; commonly approximately 45–76 mm. | Enhanced buckling resistance, controlled stress distribution, and suitability for higher-pressure formulations. | Industrial sprays, high-pressure personal-care products, and technical formulations. |
| Concave-Base Dome | Creates a recessed base that can improve stability, clearance, and interaction with packaging equipment. | Tinplate or aluminum with a suitable internal lacquer. | Deep drawing and controlled concave-base forming, followed by trimming and curling. | Typically produced for can diameters of approximately 45–65 mm. | Improved standing stability, protected bottom profile, and compatibility with automated handling lines. | Consumer aerosols, air fresheners, and products requiring stable shelf presentation. |
| Specialty Dome for Aggressive Formulations | Provides pressure closure while minimizing contact between the formulation and the metal substrate. | Aluminum or steel with an internally applied protective lacquer or laminate. | Forming followed by controlled internal coating, curing, inspection, and dimensional testing. | Manufactured in sizes matched to the can body, commonly approximately 45–76 mm. | Improved corrosion protection, coating adhesion, chemical resistance, and pressure retention. | Acidic, alkaline, solvent-based, or otherwise chemically demanding aerosol formulations. |
| Cone and Dome with Protective Coating | Provides the required structural part while protecting the metal from formulation-related corrosion. | Coated tinplate, coated steel, or lacquered aluminum. | Metal forming, internal or external coating, thermal curing, and coating inspection. | Available across common aerosol body diameters, approximately 35–76 mm. | Coating uniformity, strong adhesion, low porosity, product compatibility, and extended shelf-life potential. | Products containing water, alcohol, fragrances, solvents, or corrosion-sensitive ingredients. |
| Custom-Profile Cone or Dome | Adapts the aerosol package to a specific valve, actuator, body diameter, appearance, or filling-line requirement. | Steel or aluminum selected after pressure, compatibility, and forming evaluations. | Customer-specific tooling, multi-stage forming, trimming, curling, coating, and inspection. | Determined by the package design; common body diameters remain approximately 35–76 mm. | Tailored valve fit, unique appearance, optimized material usage, and integration with dedicated production equipment. | Specialty cosmetics, medical products, technical aerosols, and differentiated package designs. |