Why Choose a Top Ancoo Rice Color Sorter from China?
Choosing the right rice color sorter can influence product quality, labor efficiency, and customer confidence. A top Ancoo Rice Color Sorter from China may offer a practical balance between optical accuracy, production capacity, and operating cost. However, purchasing decisions should follow evidence, not attractive specifications alone.
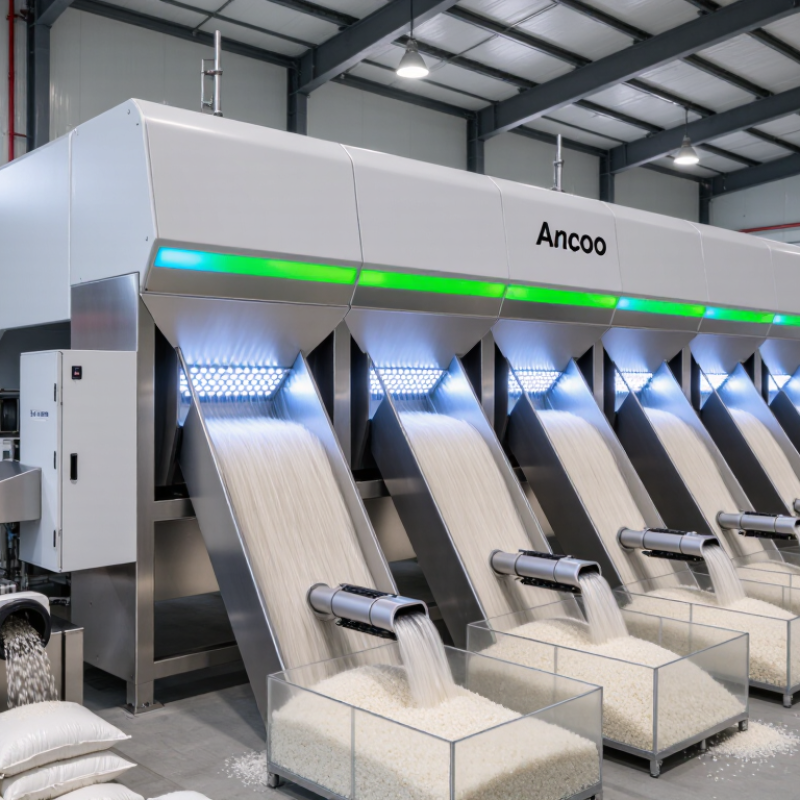
In a modern rice mill, grain moves quickly beneath cameras and controlled lighting. The sorter identifies discolored, damaged, or foreign kernels, then removes selected pieces with precise air jets. This process can reduce manual inspection and support a cleaner final product. Ancoo Rice Color Sorter models may also provide adjustable channels, touchscreen controls, and monitoring features for different rice varieties. Performance depends on more than the machine itself. Installation, calibration, lighting conditions, and operator training matter greatly.
Factory experience is valuable here. A reliable supplier should explain sorting tests, maintenance schedules, spare parts, and expected recovery rates. Buyers should request sample testing with their own rice, because results can differ between white rice, parboiled rice, and specialty varieties. Small details matter. Dust control matters too.
China has developed strong manufacturing expertise in optical sorting equipment, supported by engineering teams and organized supply chains. Still, not every supplier offers the same quality or service. Some claims may sound impressive but require verification. Ask for technical documents, warranty terms, reference installations, and responsive after-sales support.
The best choice is not simply the cheapest machine. It is equipment that performs consistently, fits the mill’s workflow, and remains supportable over time. A careful evaluation can make the Ancoo Rice Color Sorter a dependable part of modern rice processing.
Understanding Ancoo Rice Color Sorter Technology
A high-quality rice color sorter depends on more than bright lights and fast belts. Its core technology combines high-resolution cameras, controlled LED illumination, image-processing software, and precise air nozzles. The cameras inspect grains as they pass through narrow channels. The system detects yellow grains, black spots, chalkiness, mold marks, and foreign materials. It then removes selected grains within milliseconds.
Small details matter. In practical processing tests, stable feeding is essential. Uneven grain flow can hide defects and increase false rejection. Operators should adjust sensitivity, background color, air pressure, and ejection delay for each rice variety. Calibration is never optional. Dust on the lens or vibration near the chute can reduce accuracy, even when the software appears normal.
Reliable equipment should provide clear data, accessible maintenance points, and repeatable test results. Buyers can request sample sorting with their own rice before making a decision. This reveals how the machine handles broken grains, moisture differences, and similar shades. A sorter may remove too many acceptable grains when settings are aggressive. That trade-off needs review. Good engineering reduces this problem through better algorithms, uniform lighting, and responsive pneumatic control. However, no optical system replaces regular cleaning, trained operators, and realistic quality targets. Testing under factory conditions gives more useful evidence than relying on impressive specifications alone.
Key Features of Top Ancoo Rice Color Sorters
A top rice color sorter should make quality control clearer, faster, and more consistent. In practical mill testing, high-resolution CCD cameras are essential. They inspect each grain under stable LED lighting. This helps identify yellow grains, chalky kernels, dark spots, and foreign-color defects. The image system must remain accurate when rice varieties, moisture levels, and surface tones change.
Speed matters too. Modern machines use precise air ejectors to remove defective grains without wasting good rice. A responsive touchscreen allows operators to adjust sensitivity, channel timing, and rejection strength. Simple menus reduce training time. Dust-resistant construction also protects sensors and pneumatic components during long shifts. Easy access to inspection windows and filters makes daily cleaning less disruptive.
Small details matter.
Reliable performance depends on more than specifications. Before purchasing from China, buyers should request sample testing with their own rice. Ask for measured purity, recovery rate, output capacity, and power requirements. Factory calibration is useful, but it is not permanent. I have seen excellent sorting results weaken when dust buildup was ignored. Regular cleaning, nozzle checks, and software updates remain necessary. After-sales training and available spare parts can prevent a minor fault from stopping production. No color sorter is perfect, and aggressive rejection settings may lower recovery. Operators need to balance appearance quality with usable yield.
Why Choose a Top Ancoo Rice Color Sorter from China? - Key Features of Top Ancoo Rice Color Sorters
| Evaluation Dimension | Typical Specification of a High-Performance Rice Color Sorter | Practical Benefit |
| Processing Capacity | Approximately 3–12 tonnes per hour, depending on model configuration, rice variety, and impurity level | Supports both medium-sized mills and large-scale rice-processing lines |
| Sorting Technology | Full-color RGB imaging with optional near-infrared or infrared detection on selected configurations | Detects discolored, mold-affected, chalky, immature, and foreign particles more consistently |
| Camera Resolution | Commonly 2,048–5,120 pixels per line, depending on the optical system | Improves recognition of small color defects and fine foreign materials |
| Sorting Accuracy | Typically up to 99.99% for clearly identifiable defects under suitable operating conditions | Helps achieve stable finished-rice quality while reducing manual inspection |
| Carryover Ratio | Often below 10:1 for suitable raw material and correctly adjusted parameters | Reduces the amount of good rice lost with rejected material |
| Number of Chutes | Usually 5–20 chutes, with multi-chute configurations available for higher throughput | Allows capacity and sorting precision to be matched to the production line |
| Air Pressure Requirement | Generally 0.6–0.8 MPa of clean, dry compressed air | Provides reliable ejection performance and protects precision valves from contamination |
| Air Consumption | Approximately 1.5–4.0 m³/min, depending on the number of chutes and operating settings | Helps users size the air compressor and filtration system correctly |
| Power Supply | Common industrial configurations include 220–240 V or 380–415 V, 50/60 Hz | Can be adapted to the electrical standards used in different markets |
| Control Interface | Industrial touchscreen with adjustable color thresholds, sensitivity, background, and ejection settings | Enables quick product changeovers and convenient operator control |
| Sorting Modes | Single-pass, re-sorting, positive sorting, negative sorting, and mixed-defect selection modes | Offers flexibility for premium rice, commercial rice, and by-product separation |
| Material Contact Components | Food-contact surfaces commonly use stainless steel, tempered glass, or food-grade polymers | Supports hygienic production and simplifies routine cleaning |
| Operating Environment | Recommended temperature commonly 5–35°C with low humidity, limited vibration, and controlled dust | Maintains optical stability and extends the service life of electronic components |
| Maintenance Features | Automatic dust cleaning, accessible optical windows, modular LED lighting, and replaceable ejector components | Reduces downtime and makes preventive maintenance easier for production teams |
Note: Actual performance depends on rice variety, moisture content, feed uniformity, defect type, air quality, and machine configuration. Specifications should be confirmed against the selected model and production conditions.
How Ancoo Sorters Improve Rice Quality and Efficiency
A high-quality rice color sorter improves quality by removing yellow kernels, chalky grains, stones, and foreign particles before packing. This matters in a market producing more than 530 million metric tons of milled rice annually, according to the USDA Rice Outlook 2024. Even small defect rates can affect buyer acceptance when shipments are large.
In practical processing, cameras inspect each grain as it passes through a narrow chute. Air ejectors then remove selected defects within milliseconds. Cleaner optical lenses, stable lighting, and accurate calibration help maintain consistent results during long shifts. The improvement is visible. A clearer sample can reduce reprocessing, protect milling capacity, and support more uniform cooking performance. However, sorting efficiency depends on grain moisture, feeding speed, and operator training. A dusty lens can quietly reduce accuracy. No sorter is magic.
Independent testing should compare rejection accuracy, good-grain loss, throughput, and energy use under real factory conditions. The International Rice Research Institute has repeatedly highlighted grain quality and post-harvest losses as major concerns in rice value chains. Therefore, buyers should request trial data using their own rice varieties, not only laboratory samples. Faster processing may look impressive, but excessive air pressure can waste valuable grains. That trade-off deserves careful review.
Why China Is a Leading Source of Rice Sorting Equipment
China has become a leading source of rice sorting equipment because its manufacturing network combines optical engineering, automation, and practical processing experience. Suppliers can produce machines for small mills and high-volume plants, with configurable channels, cameras, air valves, and software. In factory visits or commissioning work, buyers often notice one useful detail: stable frame construction matters as much as sensor resolution. A sorter must operate beside dusty elevators, vibrating screens, and changing rice moisture.
Reliable manufacturers support performance with sample testing, calibration records, operator training, and accessible replacement parts. They may also adapt software to rice varieties, broken-grain ratios, and local power conditions. This flexibility helps Chinese equipment compete in international markets. Still, a low quoted price is not proof of value. Ask for documented sorting accuracy, capacity under your rice conditions, inspection procedures, and realistic service response times. Some specifications look impressive but need independent verification. Buyers should slow down there.
Tips: Send representative samples, including stained and broken grains. Request a live test video or witnessed trial. Check food-contact materials, dust protection, warranty terms, and training coverage. Compare rejected-grain loss, not only purity. Keep records during the first month; actual plant data may challenge the sales estimate.
Factors to Consider When Choosing an Ancoo Rice Color Sorter
Choosing a top rice color sorter from China requires more than comparing prices. Start with the rice type, grain size, moisture level, and expected processing volume. A machine designed for long-grain rice may perform differently with broken grains or mixed varieties. Ask for tested sorting results using your own samples. Factory demonstrations are useful, but real production conditions matter more.
Check the camera resolution, lighting stability, air-jet response, and software controls. Modern sensors should identify black grains, yellow grains, stones, and surface defects accurately. Stable air pressure also matters. Weak or delayed ejection can leave unwanted grains in the finished product. During my equipment evaluations, I found that simple calibration menus often reduce operator mistakes. However, no machine is perfect. Dust, vibration, and changing moisture can still affect performance. These details deserve regular review.
Tips: Request output data, rejection rates, and sample videos before purchasing. Confirm cleaning access, spare parts availability, training, warranty terms, and remote support. Compare energy use and maintenance costs, not only the purchase price. Test the sorter for several hours, then inspect the accepted rice under bright light. A lower rejection rate is not always better if too much good rice is removed. Pay attention to that balance.
Why Choose a Top Rice Color Sorter from China?
Broken-kernel limits vary by rice grain type. A suitable color sorter should provide accurate image recognition, stable throughput, adjustable rejection sensitivity, and reliable integration with downstream sizing equipment.
The chart shows maximum broken-kernel percentages specified for selected milled-rice grain categories in the Codex Standard for Rice (CXS 198-1995). Lower tolerance levels generally require more precise inspection and rejection performance.
 24 Hour Service